Operator screens
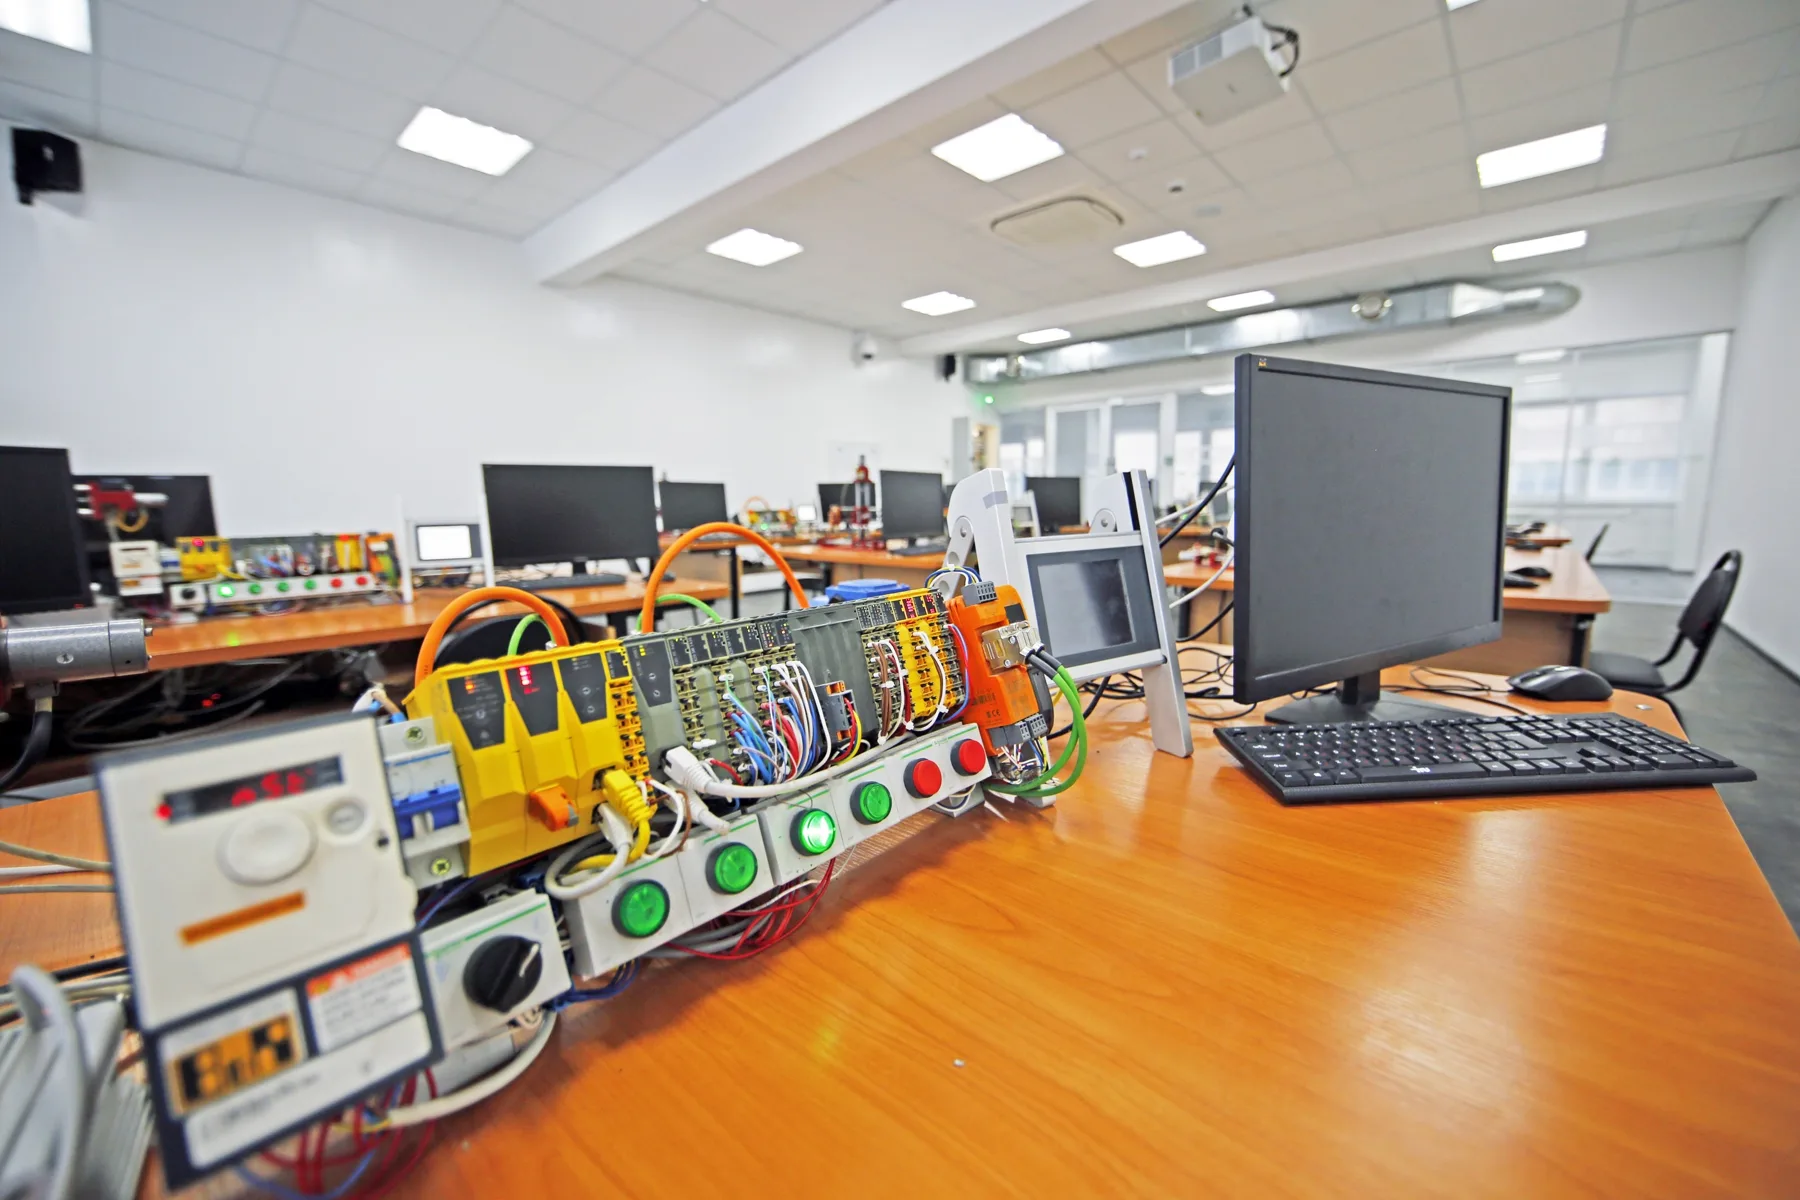
Operators see pass, reject, or hold, and the reason, at the HMI. Borderline or high-cost parts can wait for someone on your floor to confirm, and each confirmation is logged with a name and time. See How a system works.
We program and commission operator screens and robot cells with your PLC, the same way we deliver our vision stations: specified with your team, tested before startup, and handed over at site acceptance.
Problems
Operators see pass, reject, or hold, and the reason, at the HMI. Borderline or high-cost parts can wait for someone on your floor to confirm, and each confirmation is logged with a name and time. See How a system works.
A PanelView Standard or PanelView Plus 6 converted to PanelView Plus 7 in FactoryTalk View ME, bench tested, and swapped in one site day. See Legacy line rescue.
Every system connects to your PLC for rejects and line signals, and it can share data with robots, including robot pick guidance from codes and labels read on several case faces.
Your OEM or hardware supplier provides the robot and the equipment; we program and commission it. See Partners.
Controls and field wiring in one cabinet, commissioned with the rest of the cell. When a job needs field wiring, it is quoted with a licensed electrical contractor.
Results, reject records, and recipe and job data go to your MES or ERP.
How it works
Hardware, panel, I/O, and screens defined with your team. Tell us the PLC and HMI platforms in the form; we confirm before we quote.
Panel built and programs written.
Live on the line with outputs disabled. Outputs enabled after your sign-off.
Training and support after handover. Support plans cover the PLCs and HMIs on your floor, ours or someone else's.